jasonsong889@gmail.com

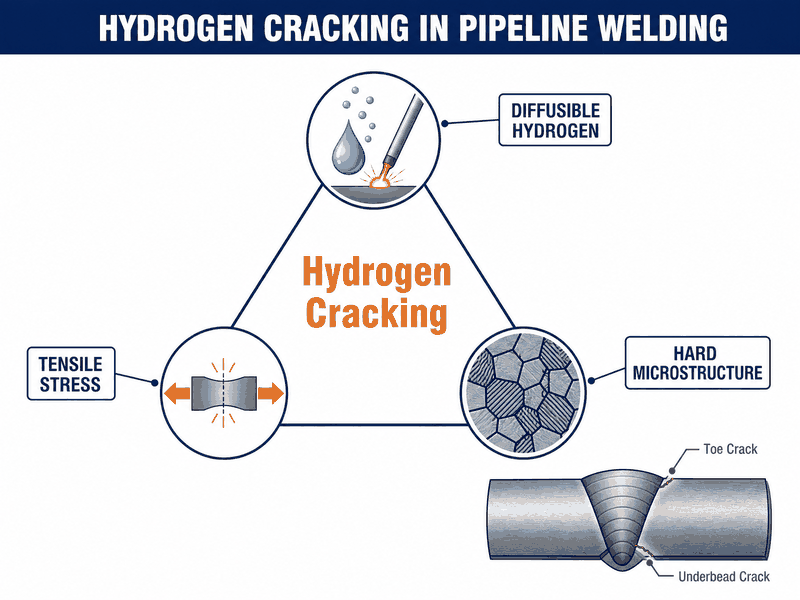
Diagram showing the three conditions that cause hydrogen cracking in pipeline welding: diffusible hydrogen, tensile stress, and a hard susceptible microstructure

How to Prevent Hydrogen Cracking in Pipeline Welding

Hydrogen cracking in pipeline welding is the delayed cold cracking failure that occurs when diffusible hydrogen, a hard susceptible microstructure, and tensile stress act together in a finished weld. You prevent it by using low-hydrogen consumables, correct preheat, interpass control, and delayed inspection so hidden cracks cannot reach service. This guide explains the hydrogen cracking mechanism, the three conditions that

How to Prevent Hydrogen Cracking in Pipeline Welding Baca Selengkapnya »
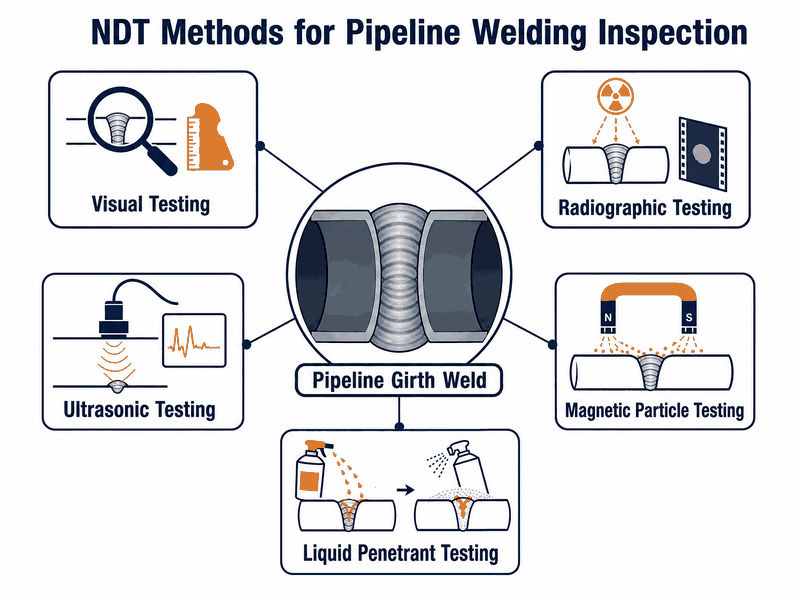
Infographic showing the five core NDT methods used in pipeline welding inspection: visual testing, radiographic testing, ultrasonic testing, magnetic particle testing, and liquid penetrant testing applied to a pipeline girth weld

Pipeline Welding Inspection Checklist: NDT Methods for Quality Assurance

A pipeline welding inspection checklist is a stage-by-stage quality plan that verifies every girth weld against the acceptance criteria of the governing code before final pipeline inspection and commissioning. It pairs visual examination with non-destructive testing (NDT) methods, specifically radiographic testing (RT), ultrasonic testing (UT), magnetic particle testing (MT), and liquid penetrant testing (PT), to

Pipeline Welding Inspection Checklist: NDT Methods for Quality Assurance Baca Selengkapnya »

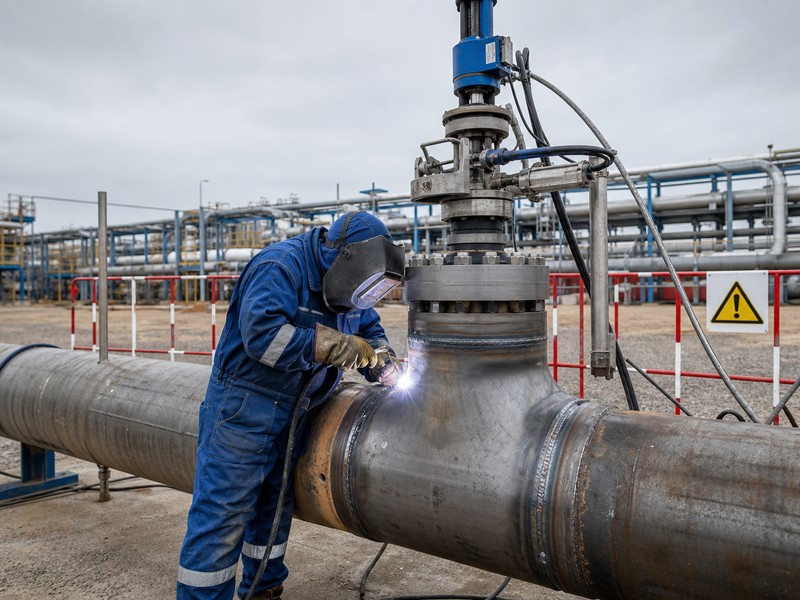
Welding technician performing in-service pipeline welding on a pressurized live pipeline with hot tap fittings and equipment

Complete Guide to In-Service Pipeline Welding

In-service pipeline welding is the controlled practice of welding onto a pressurized pipeline while it remains in operation, typically for hot tapping, line stopping, and repair connections that would otherwise force a shutdown. To weld on a live line safely, you must qualify the procedure for the actual service conditions, measure the remaining wall thickness,

Complete Guide to In-Service Pipeline Welding Baca Selengkapnya »
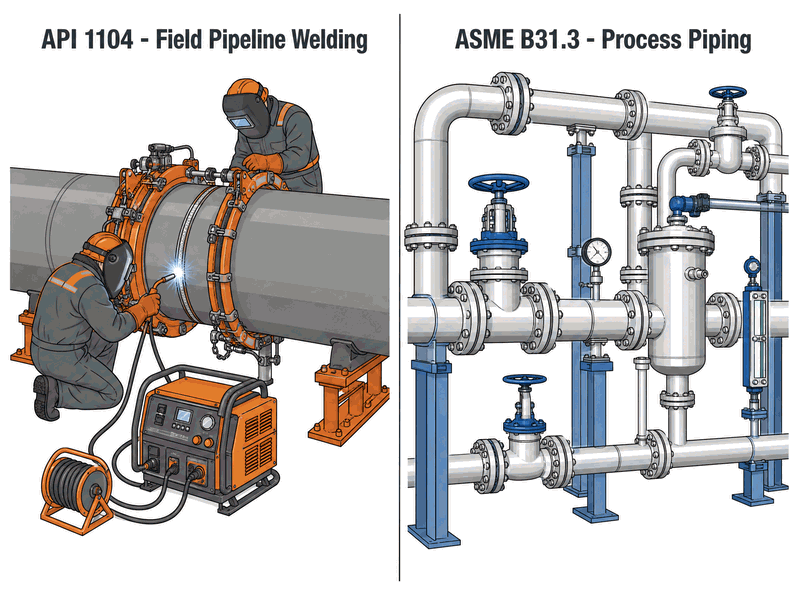
Infographic comparing API 1104 and ASME B31.3 application scopes: cross-country pipeline welding on one side and in-plant process piping on the other

API 1104 vs ASME B31.3: Which Standard Applies to Your Pipeline Project?

Deciding between API 1104 vs ASME B31.3 comes down to one question: where does your pipe sit? ASME B31.3 applies to process piping inside facilities such as refineries, chemical plants, and power stations, while API 1104 governs the field welding of cross-country pipelines built to ASME B31.4 or ASME B31.8; when a project combines both,

API 1104 vs ASME B31.3: Which Standard Applies to Your Pipeline Project? Baca Selengkapnya »

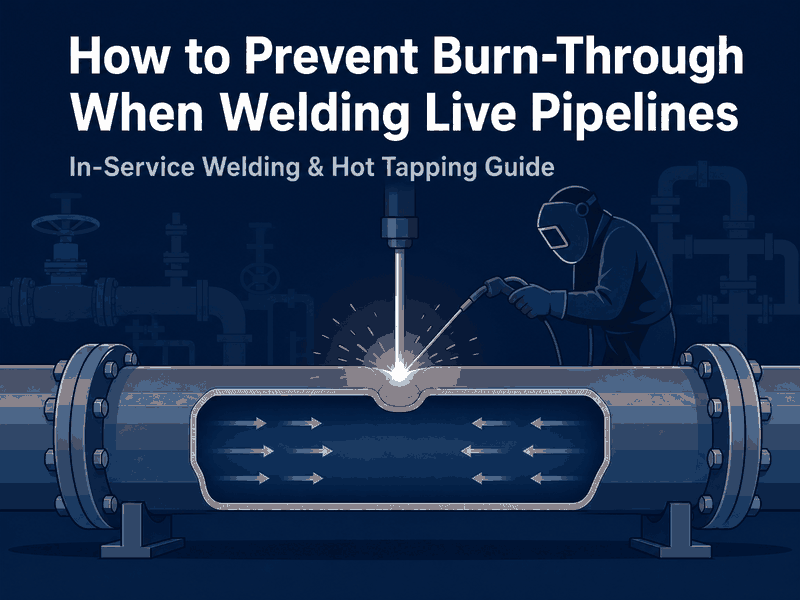
burn through prevention live pipeline welding cover

How to Prevent Burn-Through When Welding Live Pipelines

Burn-through is the failure that occurs when the weld pool melts through the remaining pipe wall of a live pipeline and the internal pressure blows out the weakened area. To prevent burn-through when welding live pipelines, you must verify the remaining wall thickness first, weld to a qualified in-service welding procedure, keep heat input low

How to Prevent Burn-Through When Welding Live Pipelines Baca Selengkapnya »

ASME superheated steam leak repair clamp JSW installation

ASME-Compliant Steam-Leak Repair Clamps for Refinery Piping: 400°C+ and 5MPa Engineering Guide

For refinery interconnecting piping handling superheated steam at 400°C+ and 5MPa, ASME Section VIII or PCC-2 compliant engineered leak repair clamps are the only certified mechanical solutions for live containment without plant shutdown. Standard elastomeric repair methods fail under these extreme thermal loads, requiring specialized graphite or mica-based sealing systems to manage thermal expansion and prevent “steam

ASME-Compliant Steam-Leak Repair Clamps for Refinery Piping: 400°C+ and 5MPa Engineering Guide Baca Selengkapnya »

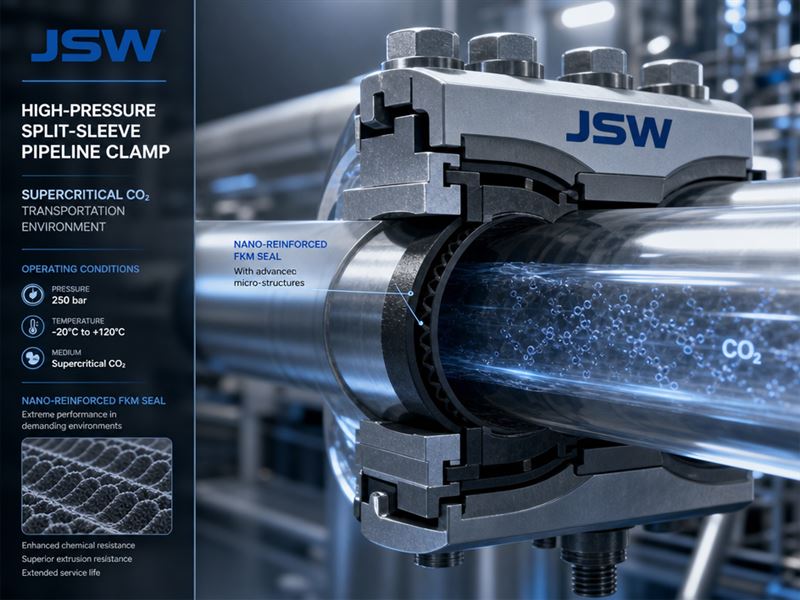
JSW high-pressure clamp with RGD-resistant seals for sCO2 pipeline repair.

sCO2 Pipeline Leak Sealing: RGD Resistance & Clamp Guide

Supercritical CO2 (sCO2) pipeline leak sealing is achieved by installing structural mechanical clamps integrated with NORSOK M-710 certified RGD-resistant seals. For CCUS infrastructure, these seals must withstand phase-change pressures exceeding 74 bar (1,070 psi). The primary sealing mechanism involves controlled radial compression that neutralizes the “explosive decompression” effect of sCO2, ensuring long-term integrity in high-pressure transport environments. This guide provides

sCO2 Pipeline Leak Sealing: RGD Resistance & Clamp Guide Baca Selengkapnya »

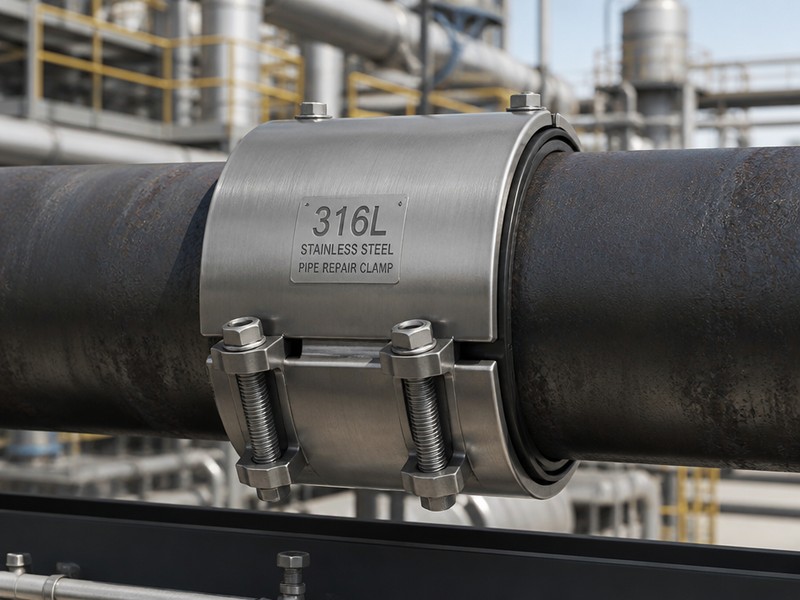
Industrial 316L stainless steel repair clamp on carbon steel pipe with NACE-compliant dielectric insulation buffer.

How to Prevent Galvanic Corrosion in Stainless Steel Clamps on Carbon Steel Pipelines?

Are you facing accelerated pipe thinning where you’ve installed stainless steel clamps? The underlying risk of Galvanic Corrosion Stainless Steel Clamps on carbon steel systems is often underestimated. To protect refinery assets, the definitive solution is dielectric isolation per NACE SP0169, utilizing non-conductive buffers like EPDM or PTFE to break the electrochemical circuit. This comprehensive guide provides technical

How to Prevent Galvanic Corrosion in Stainless Steel Clamps on Carbon Steel Pipelines? Baca Selengkapnya »

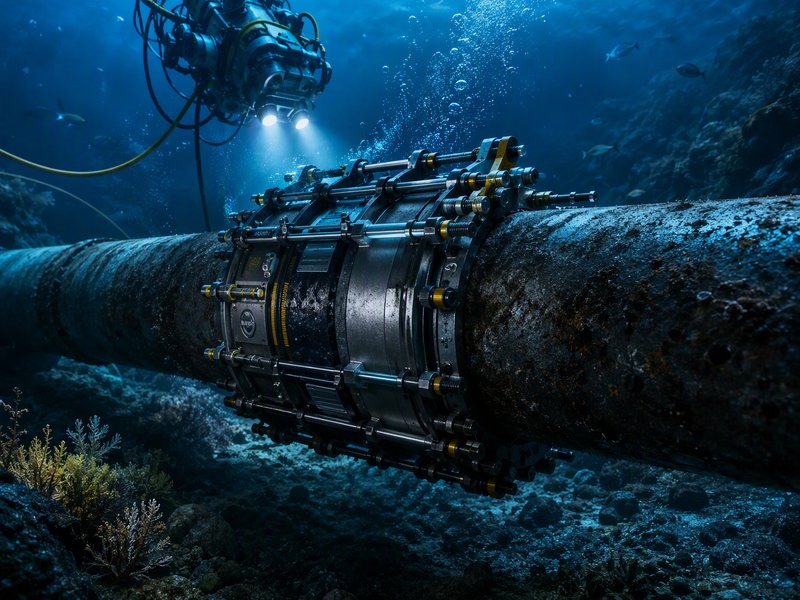
Heavy-duty structural repair clamp for subsea oil pipelines being installed by a professional ROV on the deep ocean floor, featuring high-pressure metallic housing.

Sizing and Designing Heavy-Duty Structural Repair Clamps for Subsea Oil Pipelines Under High External Hydrostatic Pressure

What is the Correct Sizing for a Subsea Pipeline Repair Clamp in High-Pressure Environments? Sizing a subsea pipeline repair clamp for deepwater (>1,000m / 3,280 ft) requires calculating the specific pressure differential between internal fluids and external hydrostatic head. In deepwater environments exceeding 1,000 meters, this sizing process is primarily dictated by the external hydrostatic pressure and the pressure

Sizing and Designing Heavy-Duty Structural Repair Clamps for Subsea Oil Pipelines Under High External Hydrostatic Pressure Baca Selengkapnya »

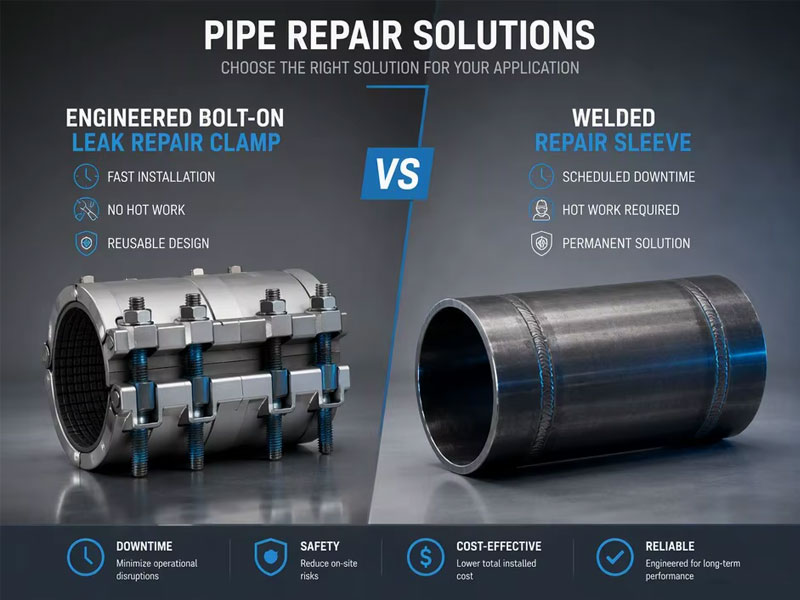
Engineered bolt-on leak repair clamp vs welded repair sleeve comparison chart highlighting differences in installation time, hotwork requirements, reusability, and cost-effectiveness for industrial pipe repair strategies.

Engineered Bolt-On Leak Repair Clamps vs. Welded Sleeves: ASME PCC-2 & API 570 Selection Criteria

1. Quick Decision: When to Choose Bolt-On Clamps over Welded Sleeves? The core answer for pipeline integrity engineers: Use Engineered Bolt-On Clamps (designed per ASME Section VIII and ASME PCC-2 Article 2.1) whenever hot work is prohibited or the remaining wall thickness (t_rem) is below 3.2mm (1/8 in). These clamps provide a 100% cold-work solution that restores 100% MAWP without the risk of burn-through.

Engineered Bolt-On Leak Repair Clamps vs. Welded Sleeves: ASME PCC-2 & API 570 Selection Criteria Baca Selengkapnya »