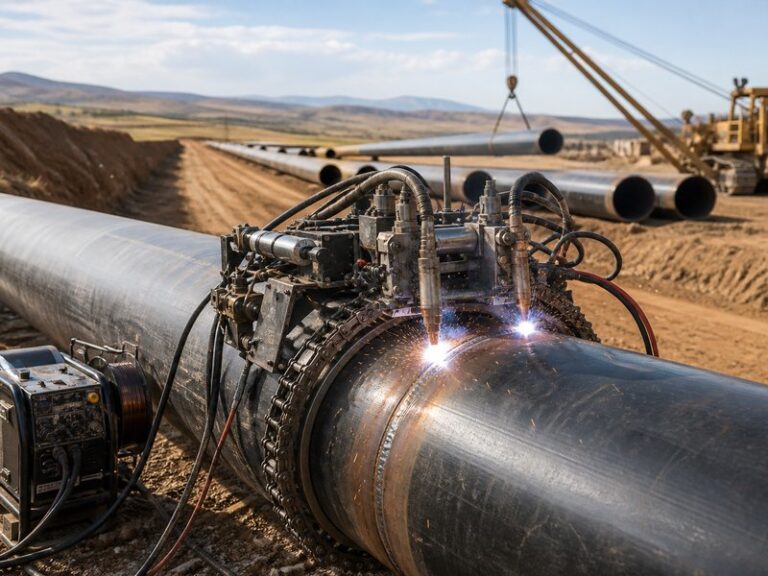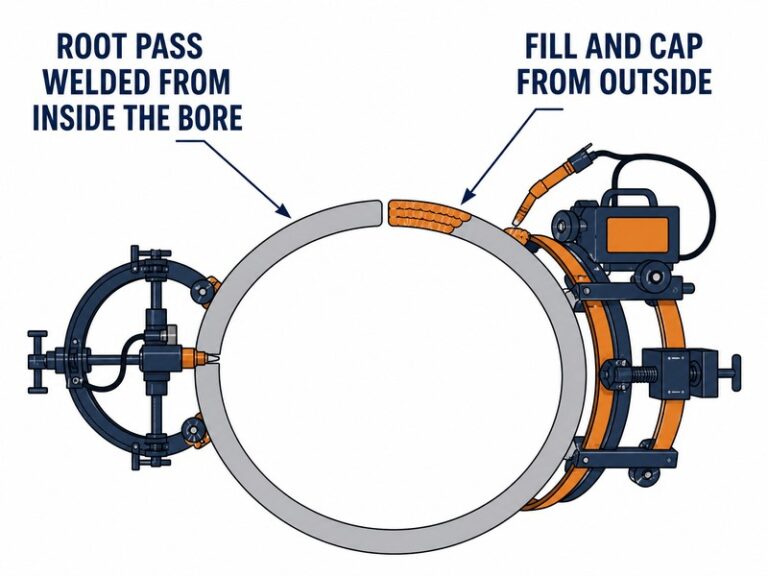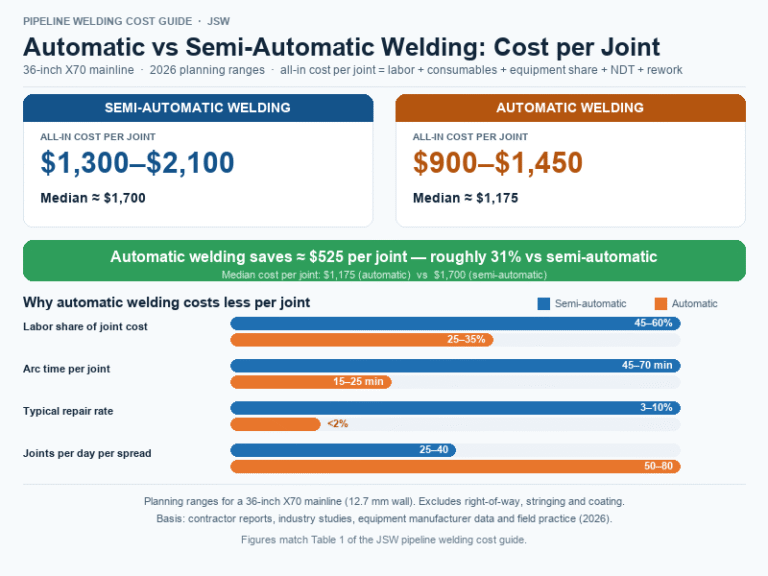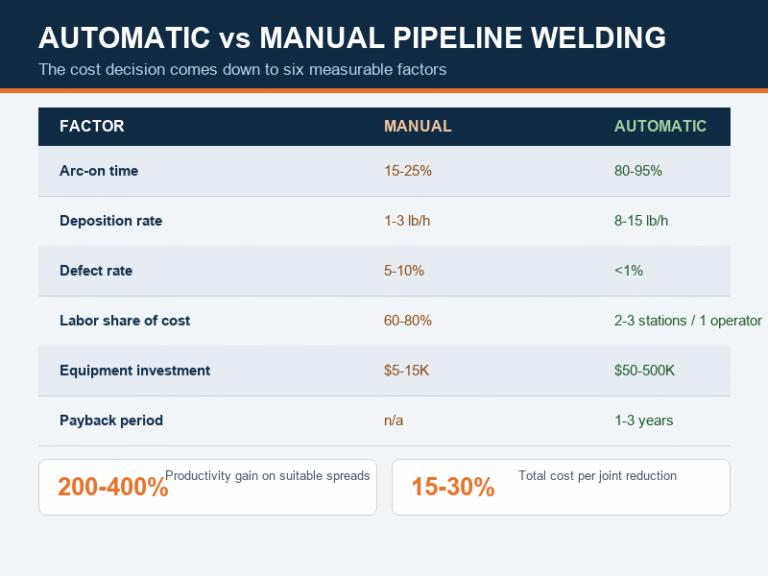
Comparison infographic of automatic welding vs manual welding for pipelines: arc-on time, deposition rate, defect rate, labor share of cost, equipment investment, and payback period on either side

Automatic Welding vs Manual Welding: Which Is More Cost-Effective?

Automatic welding vs manual welding: for new mainline construction with a high number of girth welds, automatic welding is more cost-effective, typically cutting total cost per joint by 15-30%. The advantage comes from higher deposition rates, longer arc-on time, and lower defect rates, which outweigh the higher equipment investment. For
Read More »
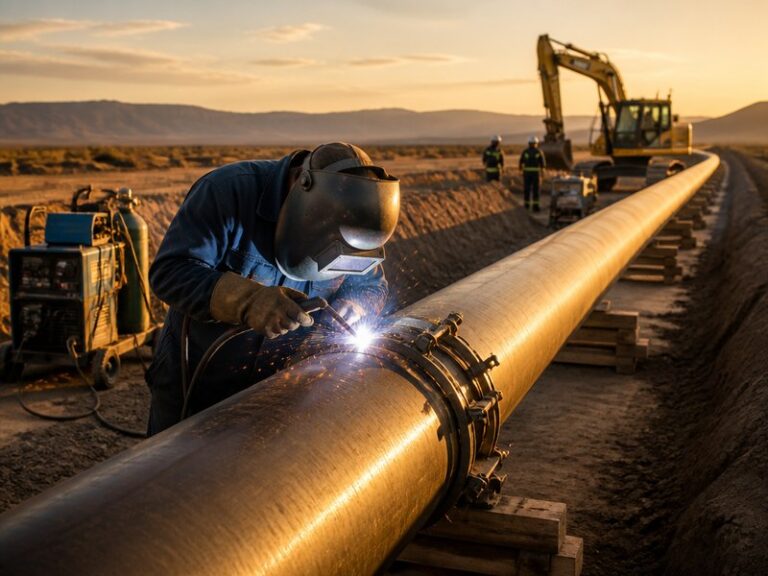
Quality audit of pipeline welding services: a welding engineer inspecting a girth weld on a large-diameter pipeline while the welding crew works on site

How to Evaluate the Quality of a Pipeline Welding Service Provider

High-quality pipeline welding services are identified by four measurable signals: a first-pass acceptance rate of 95 percent or higher, a weld repair rate below 5 percent, welding procedure specifications backed by valid procedure qualification records, and welder qualifications that match the exact process, pipe grade, and position of your project.

Read More »
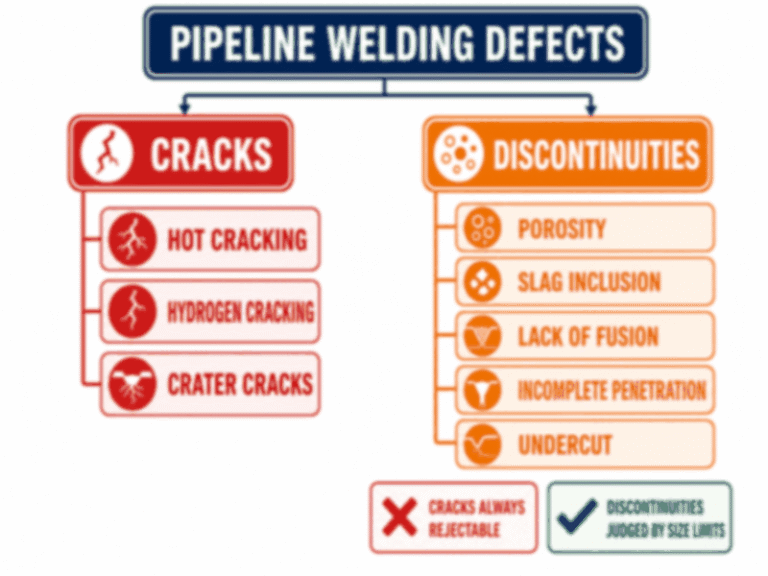
Classification diagram of common pipeline welding defects: cracks (hot cracking, hydrogen cracking, crater cracking) and discontinuities (porosity, slag inclusion, lack of fusion, incomplete penetration, undercut)

Common Pipeline Welding Defects and How to Prevent Them

Pipeline welding defects are the discontinuities that make a girth weld fail acceptance or leak in service, and the most common ones are porosity, slag inclusion, lack of fusion, incomplete penetration, and weld cracking. You prevent them by qualifying your welding procedure, controlling consumable storage and joint cleanliness, welding inside the

Read More »
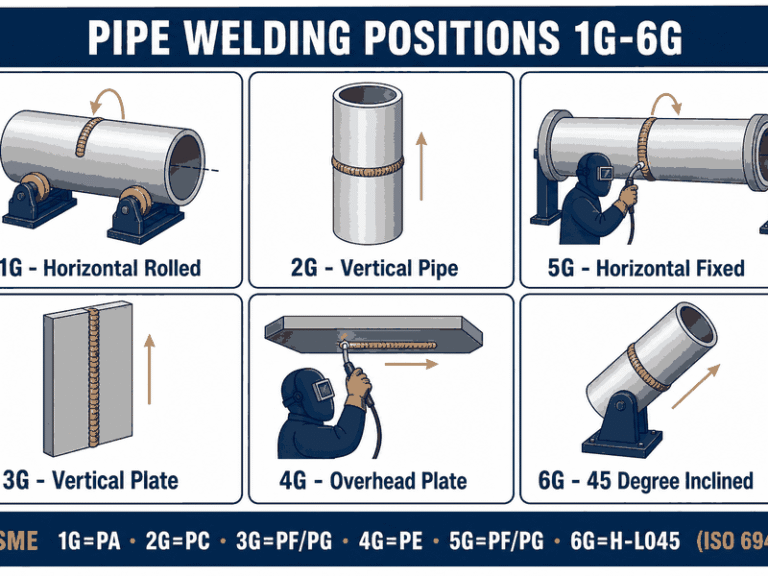
Welding position chart showing pipe positions 1G, 2G, 5G, and 6G with pipe orientation diagrams and the plate positions 3G and 4G

Pipeline Welding Positions: 1G to 6G Explained

Pipeline welding positions from 1G to 6G are the standardized orientations used to classify, test, and qualify pipe welds, with 1G (horizontal rolled), 2G (vertical pipe), 5G (horizontal fixed), and 6G (45-degree fixed) applying to pipe and 3G and 4G applying to plate. This guide explains what every pipeline welding

Read More »
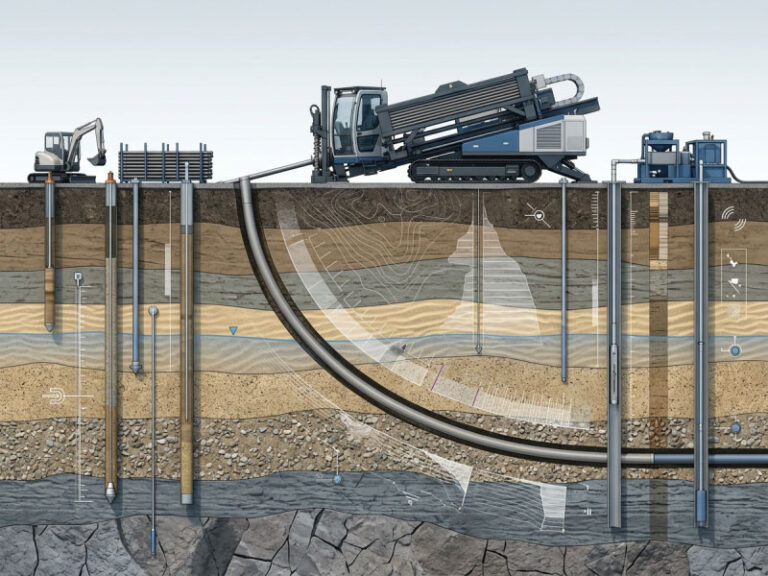
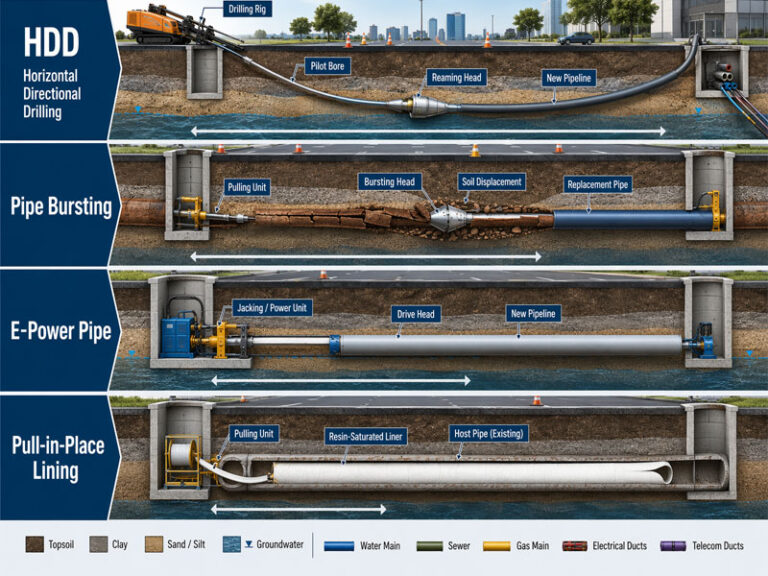
Engineering infographic comparing pulling-distance concepts for HDD, pipe bursting, E-Power Pipe, and pull-in-place lining in underground pipelines

Maximum Distance a Pipe Can Be Pulled Using Trenchless Methods: HDD Pull Length, Pipe Bursting & Lining Limits

The maximum distance a pipe can be pulled using trenchless methods ranges from approximately 50 meters to more than 3,000 meters, depending on the installation technology, pipe characteristics, ground conditions, and equipment limitations. For new pipeline construction, Horizontal Directional Drilling (HDD) typically achieves 200–800 meters per pull. For pipeline rehabilitation, specialized

Read More »
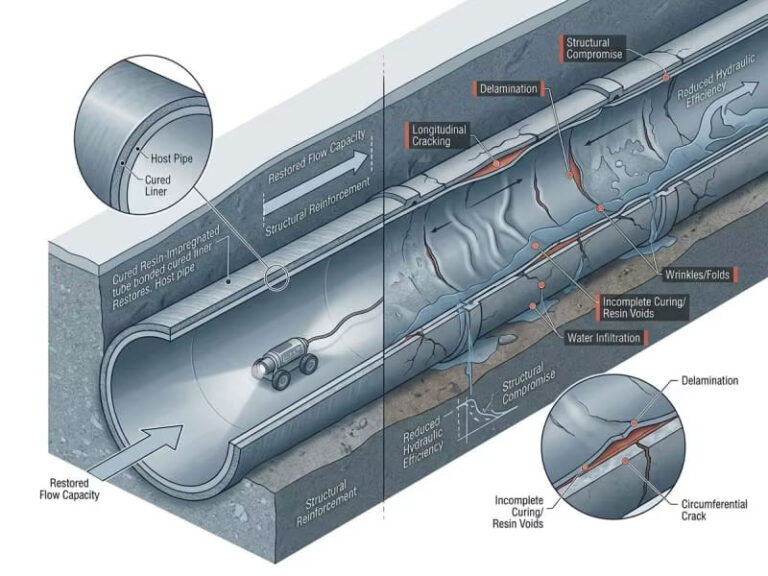
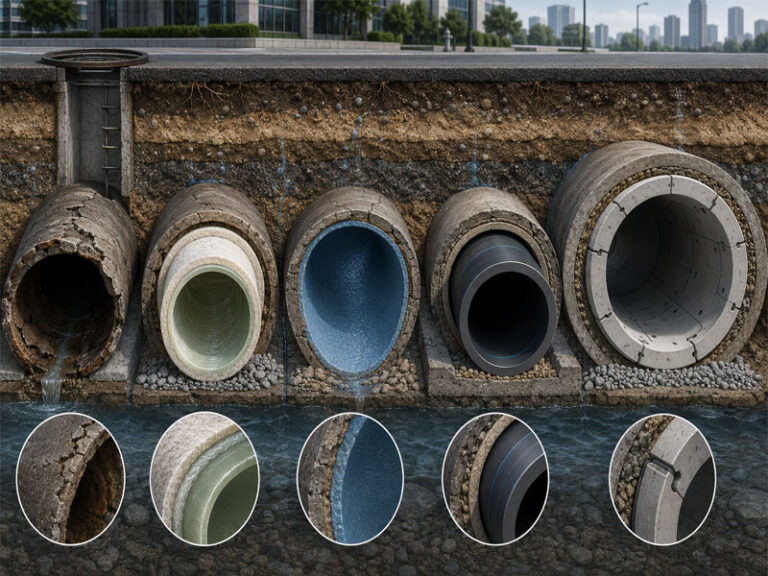
Engineering cutaway illustration comparing CIPP resin liners, spray-applied polyurea, HDPE sliplining, and UHPC structural lining segments in underground sewer pipes.

Best Trenchless Pipe Rehabilitation Materials: CIPP, Polyurea, HDPE Comparison

Best Materials for Trenchless Pipe Rehabilitation The most widely used and effective materials for trenchless pipe rehabilitation are thermosetting resin systems—specifically epoxy, polyester, and vinyl ester—combined with reinforcement fabrics such as fiberglass or polyester felt. For most municipal sewer rehabilitation projects, polyester CIPP offers the best cost-to-performance balance, while epoxy CIPP is preferred for pipes

Read More »