
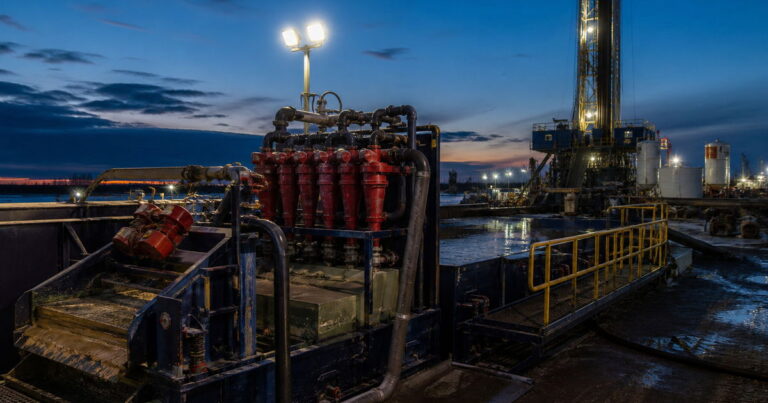
An HDD mud recycling system removes drilled solids from returning fluid so the treated fluid can be pumped back downhole, and on a large crossing that one machine decides whether the mud programme holds. The train normally runs from a catch pit through a trash pump, a shale shaker, desander and desilter hydrocyclones, and where fitted a decanter centrifuge, before clean fluid returns to a tank. This guide covers the cut point each stage delivers, sizing against the rig, screen and hydrocyclone settings, the maintenance routine and the cost case.
Which solids does an HDD mud recycling system remove, and in what order?
Why remove drilled solids before they reach the tank? Drilled solids reach the surface as coarse cuttings, sand, silt, clay and rock fines. Left in the fluid they raise unit weight and viscosity, abrade pump liners and downhole tooling, and add volume that must be handled as waste. A reclaimer removes them in stages, and every stage has a defined cut point: the particle size it can reliably reject.
A reclaimer is a solids control device rather than a mixing device, so separation is only as good as its weakest stage. The fluid side of the programme is covered in the HDD fluid science guide; this page stays on the solids-control hardware.
How does returning fluid travel from the catch pit to the clean tank?
The train is arranged so that each stage protects the equipment after it. Fluid arriving at the shaker carrying gravel will blind screens, fluid arriving at the cones carrying coarse sand will erode their apexes, and fluid reaching the clean tank carrying silt will simply be pumped back downhole.

Used fluid discharges into a catch basin, and a submersible trash pump then feeds the shaker at a steady rate while the pit ahead of it keeps stones out of the impeller. The shale shaker is the first mechanical stage. It separates solids down to roughly 200 microns and carries the bulk of the cuttings load. Hydrocyclone desanders and desilters work a finer band of roughly 25 to 250 microns, with the finer cyclone bank cutting around 20 to 25 microns, and a decanter centrifuge, where fitted, reaches roughly 2 to 5 microns.
The clean fluid then returns to a partitioned tank with mud guns and top-mounted agitators that stop heavy solids stratifying, and additives are returned through an on-board jet-shear mixing hopper.
| Scène | Typical cut point | What it protects |
|---|---|---|
| Catch pit or settling pit | Gravity settling; no fixed cut point | Buffers surge volume and drops gravel before the pump |
| Submersible trash pump | Suction strainer only | Holds steady feed to the shaker and prevents starvation |
| Shale shaker | First pass, roughly 200 microns | Removes bulk cuttings before they blind or load the cones |
| Desander hydrocyclones | Coarser end of the 25 to 250 micron band | Removes sand that would settle in the bore and abrade pumps |
| Desilter hydrocyclones | Around 20 to 25 microns | Removes silt that raises density and builds a cuttings bed |
| Decanter centrifuge, where fitted | Roughly 2 to 5 microns | Removes colloidal fines no screen or cyclone can take out |
| Clean tank, mud guns, agitators | No separation; homogenisation only | Prevents stratification so the rig sees consistent fluid |
| Jet-shear mixing hopper | Additive hydration | Prevents fish-eyes and restores weight and viscosity |
| Transfer pump | Aucun | Delivers treated fluid at the rate the borehole requires |
The cut points matter because the mud programme is written around a density and viscosity band, not around a wish to be clean, and it is fines accumulating in the clean tank that move that band.
How do I size a mud reclaimer for a rig pumping 600 gpm?
Sizing an HDD mud recycling system starts with the rig’s maximum flow rate rather than its average. The rule of thumb is to multiply rig flow rate by two when selecting reclaimer capacity, and the margin is not padding: it covers the surge during a reaming pass, the extra residence time needed when fluid returns thicker than target, and the loss of screen area the moment cuttings load a panel.
A representative packaged unit processes up to 600 gpm and separates down to 25 microns, a realistic benchmark for the middle of the large-crossing range rather than a ceiling. Undersizing shows up as fluid backing up in the catch pit, screens running wet with solids riding over the end, manifolds starved of pressure and a clean tank that slowly gains weight. Running the shaker faster rarely helps, because throughput is governed by open screen area and the fluid’s ability to pass through it.
Shale Shaker Screens: API Rating, Mesh Count and Panel Selection
Screens are rated by API rating or by mesh count, and shakers come in two-, four- or six-panel double-deck configurations. The screen is the only adjustable element in the train that changes the cut point of the whole HDD mud recycling system, so screen cut is logged against the fitted panel’s published API rating or mesh count rather than a target set on site.
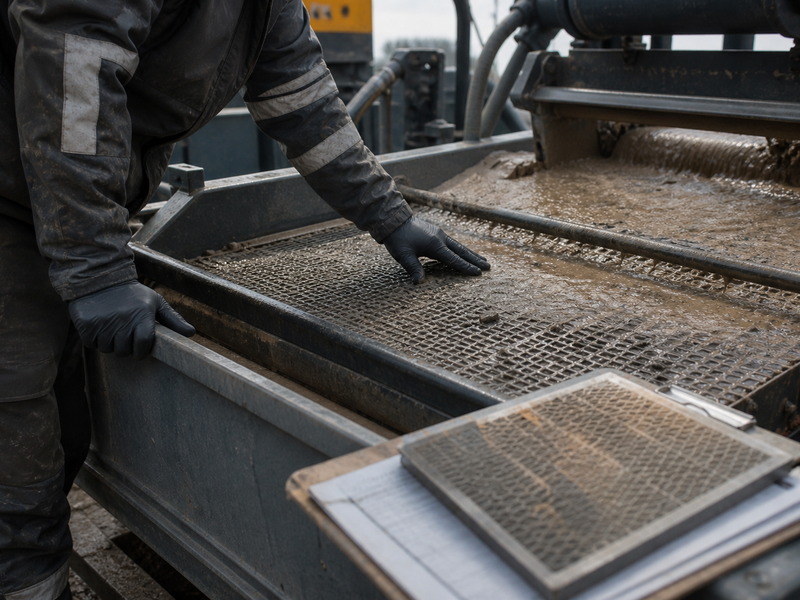
The trade-off is straightforward. A finer screen removes smaller solids but passes less fluid and blinds sooner, particularly in reactive clay where fluid can smear the mesh. A coarser screen keeps the deck dry but pushes sand onto the cones, which are usually not sized to accept it.
The screen specification is often left to the crew to decide on the day, which is how cut points drift out of the fluid programme. The practical rule is to run the finest screen the flow can carry without flooding the deck, step back one panel size if the pit rises, and log every panel by mesh hours.
Why does my desilter stop cutting solids halfway through a reaming pass?
Hydrocyclones separate solids by centrifugal force, so on an HDD mud recycling system they only work inside a feed-pressure window. Below it the cones stop classifying and simply pass the slurry; the manifold gauge is the cheapest instrument on the spread and the one most often ignored.
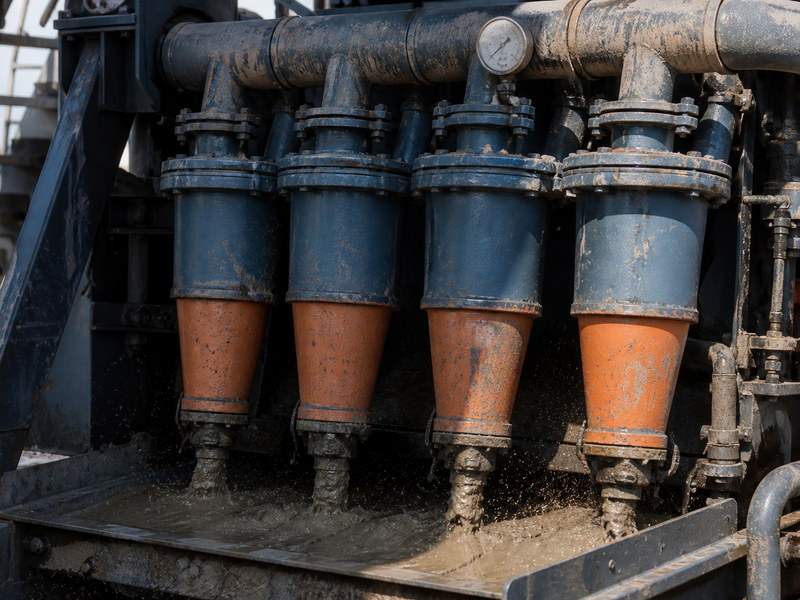
Apex condition is the second failure mode. Erosion opens the apex, and once it is oversized the cone short-circuits and rejects nothing useful. A steady spray cone means separation is happening, while a rope of solids hanging from the apex means the underflow is overloaded.
Apex condition matters on the desander bank as much as on the finer cyclone bank. Worn liners and gaskets have the same effect even when the gauge reads correctly, which is why apex inspection belongs on the schedule. Cycling the feed pump to suit the rig’s demands lets fines recirculate for hours before anyone sees the weight creep up.
The Daily, Weekly and Per-Crossing Maintenance Routine
An HDD mud recycling system stays inside its fluid programme through routine, not reaction. Because large-crossing work often runs around the clock, the schedule has to survive a shift handover without a verbal briefing being the only record. Every check below carries an acceptance indicator, so the decision to act is not opinion.
| Frequency | Task | Acceptance indicator / action |
|---|---|---|
| Daily, each shift | Inspect shaker panels for tears, holes and blanked areas; confirm the fitted mesh rating | No tear or bypass; fitted panel matches the programme and is logged |
| Daily, each shift | Read cyclone manifold feed pressure against the set point | Stable pressure inside the cone’s working range |
| Daily, each shift | Watch desander and desilter discharge patterns | Steady spray cone; investigate roping |
| Daily, each shift | Flush the trash pump strainer and check the impeller | Free flow without surging; no gravel at the intake |
| Daily, each shift | Check clean tank level, transfer pump output and pit balance | Pit volume stable; no net gain from retained solids |
| Daily, each shift | Test clean fluid for weight, gel strength and viscosity | Inside the programme band; correct via the jet-shear hopper |
| Weekly | Inspect cones, liners, gaskets and apexes for erosion | No grooving or oval apex bore; replace worn sets together |
| Weekly | Grease shaker bearings; check motor mounts and drive belts | No abnormal noise or heat; vibration within maker’s limit |
| Weekly | Check centrifuge bowl wear, scroll and differential speed | Solids discharge dry and consistent; no bowl imbalance |
| Per crossing, at shutdown | Replace screens; strip, clean and inspect the deck assembly | Full open screen area restored on every panel position |
| Per crossing, at shutdown | Replace apexes, liners and gaskets; inspect cones internally | Cut point restored towards the 20 to 25 micron finer-cone target |
| Per crossing, at shutdown | Desludge tanks and pits; review the solids control and disposal records | Tank free of settled solids; records ready for the next crossing |
Two habits make the maintenance schedule work: every check has a number attached to it, and the record travels with the equipment.
- Mid-size contractor on a multi-crossing programme: the record travels with the machine, because a reclaimer arriving with an unlogged apex change starts the next crossing behind.
- Small crew renting a packaged unit: set the trigger values with the rental supplier at rig-up, because thresholds copied from another site do not transfer.
- Site with restricted disposal: treat clean-tank weight as a cost metric as well as a quality metric, because disposal here is priced by volume.
Condition Indicators That Predict Failure Before It Stops the Crossing
Most HDD mud recycling system failures are visible for hours before the equipment actually stops working. Our field teams record the indicators below, and treating any two together as a trigger for intervention has prevented more downtime than any single alarm.
- Rising cyclone pressure at steady feed: usually a partly blinded screen or a choked cone inlet.
- Wet, runny shaker discharge: the deck is overloaded or the fluid too thick to pass the mesh.
- Roping at a cone apex: the underflow is overloaded or the apex has worn open, so separation has stopped while the unit still runs.
- Clean tank gaining weight through the shift: fines are building faster than the train removes them.
- Falling transfer pump output with rising motor current: abrasive wear or a part-blocked line, and a predictor of seal failure.
- New vibration or heat at shaker bearings or centrifuge: bearing degradation, which escalates within a shift rather than over days.
Thresholds depend on the machine and on the fluid programme, so the numbers should be set per spread at rig-up rather than copied between sites, and agreed with the rig crew before the reaming passes begin.
A decanter centrifuge moves from optional to necessary when two conditions hold at once: the fluid must be held light for borehole stability, and disposal is restricted or expensive. Where neither holds, a shaker plus hydrocyclone desander and desilter bank usually keeps the programme in band, provided the screens are changed on the schedule and the cones are kept inside their feed-pressure window. Where only disposal is the constraint, extra pit volume and a tighter shaker screen are the cheaper first step.
The Cost Case: Mud, Pumps, Bit Life, Rate of Penetration and Disposal
What does recycling actually save over a full campaign? The published benefits are lower mud cost, longer life of mud pumps and bits, higher rate of penetration, and lower disposal cost. Each has a different mechanism, and together they make solids control on a long crossing a commercial decision rather than a housekeeping one.
Mud cost falls because additive is not consumed on every barrel, and disposal falls in the same proportion: every barrel reused is a barrel that does not have to be vacuumed, tested as waste and paid for. Pump and bit life and penetration rate are linked through abrasion, since sand left in the fluid grinds pump liners, impellers and reamer cutters and shows up as spare parts and unplanned stops.
The counter-argument is footprint, power, maintenance labour and consumable parts. Applies to crossings where solids loading is continuous and disposal is priced: a reclaimer earns its footprint through mud, pump, bit and disposal savings on long, large or abrasive crossings, and on a very short bore in clean, stable ground it is a cost rather than a saving. A reclaimer also treats fluid; it does not rebuild an additive package that has already been consumed. The case strengthens with crossing length, diameter, reactive or abrasive ground, and any site where disposal is expensive or restricted.
Questions fréquemment posées
What does an HDD mud recycling system remove from drilling fluid?
An HDD mud recycling system removes drilled solids down to the cut point of its finest installed stage; below that, fines stay in circulation and return downhole.
How do I size a mud reclaimer for a large crossing?
Start with the rig’s maximum pump output and multiply by two. A packaged unit processing up to 600 gpm and cutting to 25 microns is typical of the mid-range.
How often should I change shale shaker screens while the fluid returns thicker than target?
Every shift, and again after every reaming pass. A torn or blinded panel stops removing the coarse fraction the hydrocyclones cannot accept.
Why does a desander or desilter stop separating solids?
Usually because feed pressure has fallen below the cone’s working range or the apex has worn open, letting material short-circuit straight through.
Is a decanter centrifuge necessary on a large HDD crossing?
Not on every crossing, but it becomes hard to avoid where the fluid must be kept light or disposal volume is expensive. It reaches roughly 2 to 5 microns.
What does a mud reclaimer actually save on a long, large-diameter crossing?
The saving is real but conditional on solids control working: mud, pumps, bits and disposal improve together, not on their own.
Can recycled fluid be sent back downhole without being retested?
No. Fluid in the clean tank must be tested for weight, gel strength and viscosity, because recycled fluid carrying fines can read correctly on viscosity while being heavier than the programme allows.
Points clés à retenir
- An HDD mud recycling system removes solids in stages, with cut points of roughly 200 microns at the shaker, 25 to 250 microns across the hydrocyclones, 20 to 25 microns at the desilter and 2 to 5 microns at a decanter centrifuge.
- Size the unit on rig flow rate multiplied by two; a packaged unit processing up to 600 gpm and cutting to 25 microns is typical of the mid-range.
- Screens are rated by API rating or mesh count, and the screen is the only adjustable element that changes the cut point of the whole train.
- Hydrocyclone performance is decided by feed pressure and apex condition, so roping discharge is a separation failure rather than a cosmetic issue.
- The cost case holds where the bore is long, the ground abrasive or reactive, and disposal is priced by volume.
How JSW Supports Mud Recycling on HDD Crossings
JSW is a pipeline engineering and construction company that executes trenchless crossings with its own crews and equipment. Our scope covers HDD crossing services, technologies sans tranchée for road, rail, watercourse and utility crossings, services d'installation de pipelines, follow-on pipeline inspection service work, and emergency response and contingency maintenance when a crossing or tie-in needs immediate recovery.
We plan solids control as part of the crossing rather than a service item bolted on afterwards, because on a large bore the HDD mud recycling system decides whether the fluid programme stays inside its density and viscosity bands. Reclaimer capacity, screen selection and disposal routing are costed together at bid stage, and process data from the spread is recorded so the next crossing inherits a baseline rather than an assumption.
- One contractor, one scope: engineering, fluids planning, drilling crews, equipment and restoration under one contract, so cut points and disposal volumes sit in one budget.
- Shift records you can audit: shift records of screen rating, manifold pressure, apex condition and clean-tank properties.
- Disposal priced up front: inadvertent-return plans, containment and disposal costs stated in the bid, with the assumptions visible to the owner.
- Guidance-led methods: work planned around recognised guidance including the NASTT HDD Good Practices Guidelines and applicable OSHA requirements.
Planning a large crossing and unsure how much reclaimer capacity your bore actually needs? Send your bore plan, rig pump output, ground conditions and disposal constraints for a free technical review. Our engineers respond with a scoped reclaimer and solids-control recommendation, plus a budget range.





































 English
 Arabic
 Russian
 Spanish
 French
 Vietnamese
 Polish
 Thai
 Indonesian
 Turkish
 Portuguese