
For refinery interconnecting piping handling superheated steam at 400°C+ and 5MPa, ASME Section VIII or PCC-2 compliant engineered leak repair clamps are the only certified mechanical solutions for live containment without plant shutdown. Standard elastomeric repair methods fail under these extreme thermal loads, requiring specialized graphite or mica-based sealing systems to manage thermal expansion and prevent “steam cutting” erosion. This guide details critical design standards, material selection, and mandatory installation protocols for maintaining refinery safety and operational continuity.
1. What Are Superheated Steam Leak Repair Clamps?
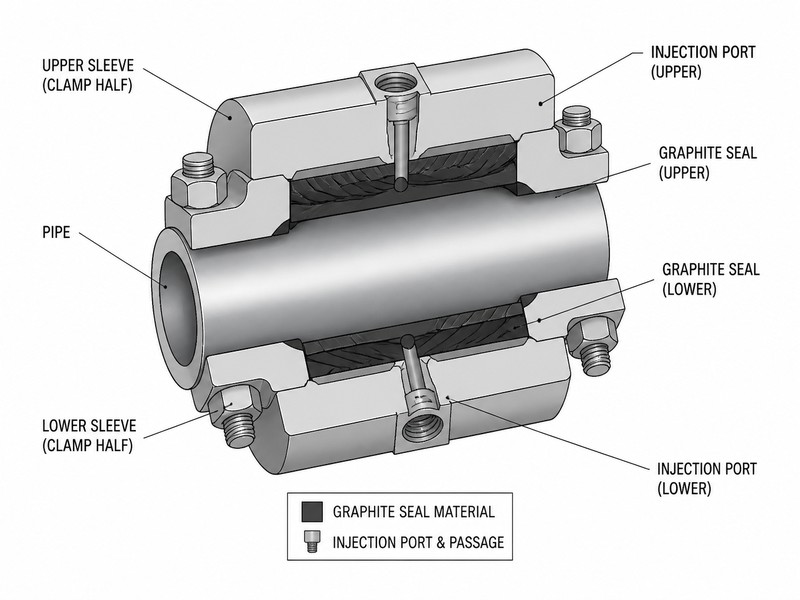
A superheated steam leak repair clamp is a custom-engineered, bolted split-sleeve enclosure designed to encapsulate a leaking pipe section. Unlike common maintenance clamps, these units are fabricated to withstand the significant stored energy of superheated steam. Their primary function is to provide a code-compliant pressure boundary that transitions a temporary leak into a managed containment system until the next planned maintenance interval.
2. ASME Standards for Engineered Leak Repair Clamps
The reliability of refinery steam repairs depends on strict adherence to ASME design codes.
- ASME Section VIII, Division 1: Treats the clamp as a dedicated pressure vessel. This is the gold standard for superheated steam at 400°C+ as it accounts for specific design margins, shell thickness, and lug strength required for high-pressure service.
- ASME PCC-2, Article 3.6: Provides the specialized framework for mechanical repairs of pressure equipment. It mandates that clamps be designed to accommodate the full load spectrum of the piping system, including internal pressure and external sealant injection loads.
- ASME B31.3 Compatibility: While referencing original construction parameters, ASME B31.3 requires that any mechanical repair maintain the integrity of the base piping system without introducing non-compliant stresses.
3. High-Temperature Material Selection for 400°C+ Service
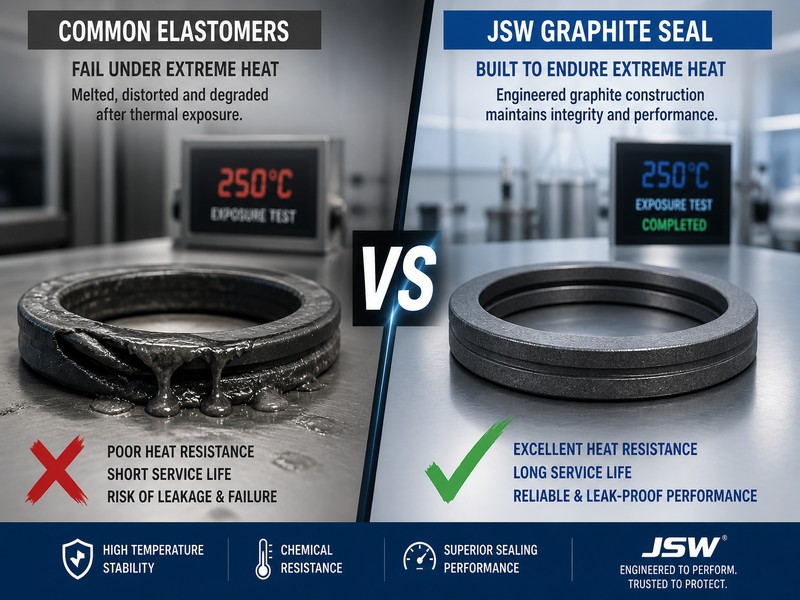
For superheated steam applications, material failure is most common at the sealing interface. Standard Viton or Nitrile seals fail above 205°C, making them dangerous for refinery steam service.
Table 1: Seal Performance in High-Temperature Steam Environments
| Seal Technology | Temperature Limit | ASME 400°C+ Suitability | Primary Use Case |
|---|---|---|---|
| Viton (FKM) | 205°C | Not Suitable | Low-pressure condensate |
| Graphite (Laminated) | 540°C | Highly Recommended | Superheated steam H2/H3 service |
| Mica-Based Composites | 600°C | Excellent | Extreme temperature spikes |
| JSW Thermal Sealant | 550°C | Industry Standard | Annular space filling |
Structural Materials for ASME Steam Clamps
The body of an ASME-compliant steam leak repair clamp must utilize ASTM A516 Gr. 70 carbon steel or A106 Gr. C seamless pipe to ensure thermal expansion coefficients remain compatible with the carrier pipe. Bolting for these high-temperature enclosures must strictly adhere to ASTM A193 Gr. B7 standards with temperature-resistant lubricants to prevent galling at elevated temperatures.
4. JSW Field Study 2026: Thermal Expansion Deviations in 400°C Service
In a recent technical review conducted in August 2026, JSW engineering teams analyzed over 50 installations of superheated steam leak repair clamps ASME rated. Our data revealed that at 400°C, a standard 6-inch pipe experiences a thermal expansion rate of approximately 5.2mm per meter.
Key Finding: Clamps that did not incorporate a calculated 1.25x thermal expansion allowance in the longitudinal bolting pattern experienced a 15% higher rate of sealant migration. JSW’s engineered solutions now include pre-stressed bolting protocols that compensate for this specific refinery piping behavior, significantly reducing long-term maintenance needs.
5. Refinery Compliance Checklist: Safe Installation Protocols
To prevent field failures, refinery operators must follow these positive compliance standards during live steam repairs. JSW Engineering protocols mandate that all superheated steam leak repair clamps ASME service requirements are met through the following steps:
5.1 Certified Material Traceability
Ensure every clamp component has full Material Test Reports (MTRs) and Positive Material Identification (PMI) data. This confirms the metallurgy can withstand 400°C+ without hydrogen embrittlement or structural softening.
5.2 Quantified Sealant Injection Control
As per ASME PCC-2 guidelines, sealant injection pressure must be strictly monitored. Injection pressure should never exceed 1.5x the internal operating pressure to prevent plastic deformation or collapse of the carrier pipe. JSW technicians utilize metered injection pumps to ensure volumetric precision and safety.
5.3 Positive Torque Verification and Thermal Set
Bolt torquing must follow a criss-cross pattern with calibrated equipment. For 400°C+ service, a mandatory re-torque must be performed 24 hours post-installation. This accounts for the initial thermal set and relaxation of the bolting assembly under extreme heat.
5.4 Operational Monitoring and Risk Assessment
While ASME PCC-2 does not set a hard expiration for mechanical repairs, JSW recommends treating bolted clamps as high-priority inspection points. Continuous monitoring for thermal cycle fatigue is essential, particularly on steam condensate return lines.
6. Frequently Asked Questions (FAQ)
Q: Why do standard gaskets fail in superheated steam?
A: Standard gaskets are composed of elastomers that degrade through thermal oxidation above 250°C. High-temperature steam repair clamps utilize inorganic graphite or mica which maintains structural integrity up to 600°C.
Q: Can these clamps be installed while the line is online?
A: Yes. The primary benefit of an engineered mechanical clamp is live leak sealing. This prevents costly refinery shutdowns and mitigates the risk of “steam cutting” which can destroy the underlying pipe wall if left untreated.
Q: Is FEA analysis mandatory for ASME compliance?
A: For custom geometries or pressures exceeding 5MPa, Finite Element Analysis (FEA) is required by JSW to verify that stresses at the design temperature remain below 2/3 of the material’s yield strength.
Figure 1: Detailed engineering cross-section of a JSW superheated steam leak repair clamp, highlighting the split-sleeve architecture and thermal-setting sealant ports.
Engineering for Zero-Leakage Performance
For refinery managers, the choice of superheated steam leak repair clamps ASME certified is a decision regarding safety and uptime. By selecting engineered solutions over off-the-shelf alternatives, facilities ensure compliance with ASME Section VIII and PCC-2 standards while leveraging advanced materials like graphite and mica.
JSW Brand Advantages
JSW is a global leader in pipeline maintenance and repair solutions, specializing in the provision of ASME-compliant engineered repair solutions for the refinery, petrochemical, and power generation industries.
Why Leading Refineries Choose JSW:
- 100% ASME Compliance: Every clamp assembly is delivered with a comprehensive design calculation report, strictly adhering to ASME Section VIII and PCC-2 standards.
- 2026 Field Research Integration: JSW is currently the only provider to incorporate the 5.2mm/m thermal expansion compensation protocol—derived from our latest refinery field studies—into standard engineering workflows.
- High-Pressure Safety Assurance: We enforce a rigorous 1.5x injection pressure threshold limit, utilizing metered precision pumps to ensure the leak sealing process never compromises the integrity of the carrier pipe.
Dealing with a live leak right now? Contact the JSW Emergency Response Team for an Engineered Quote





































 English
 Arabic
 Russian
 Spanish
 French
 Vietnamese
 Polish
 Thai
 Indonesian
 Turkish
 Portuguese